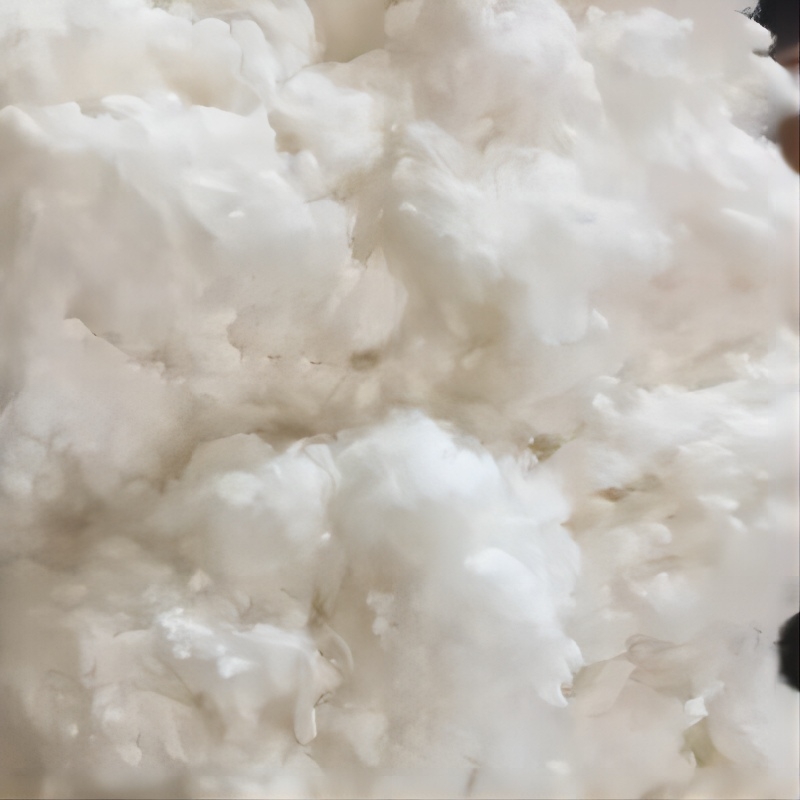
Cotton Linter Pulp: What You Need to Know About This Versatile Material
Cotton linter pulp is a versatile and sustainable raw material derived from cotton linter, a by-product of the cotton ginning process. This unique and eco-friendly material has a wide range of applications, from the production of high-quality paper and textiles to the development of innovative and sustainable new products.One company that has been at the forefront of leveraging the potential of cotton linter pulp is {}. With a strong commitment to sustainability and innovation, the company has been leading the way in developing new and exciting applications for this unique raw material.Founded in {}, {} has quickly established itself as a leader in the field of sustainable materials and product development. The company’s dedication to quality, innovation, and sustainability has set it apart from its competitors and has made it a trusted partner for businesses across a wide range of industries.One of the key strengths of {} is its ability to harness the potential of cotton linter pulp and transform it into high-quality, sustainable products that meet the needs of today’s market. By working closely with suppliers and manufacturers, {} has been able to develop a range of innovative products that offer unique benefits and advantages over traditional materials.One of the primary uses of cotton linter pulp is in the production of high-quality paper products. Thanks to its long, strong fibers and exceptional purity, cotton linter pulp is an ideal raw material for manufacturing a wide range of paper products, including printing and writing papers, specialty papers, and tissue products. By utilizing cotton linter pulp in their paper production, {} is able to create superior products that offer improved performance, sustainability, and environmental benefits.In addition to paper products, {} has also been exploring new and innovative applications for cotton linter pulp in other industries. For example, the company has been working on developing cotton linter pulp-based materials for use in the textile industry. By leveraging the unique properties of cotton linter pulp, {} has been able to create sustainable and high-performance fabrics that offer unique advantages over traditional textiles.Furthermore, {} has been exploring the potential of cotton linter pulp in the development of innovative new products in the packaging and biodegradable plastic industries. By using cotton linter pulp as a raw material, the company has been able to create sustainable and biodegradable packaging materials that offer a viable alternative to traditional plastic packaging.In addition to its innovative product development efforts, {} has also been a leader in promoting the sustainable and ethical production of cotton linter pulp. The company works closely with cotton farmers and suppliers to ensure that the raw materials used in its products are sustainably sourced and produced in an environmentally responsible manner.Through its commitment to sustainability, innovation, and quality, {} has been able to carve out a unique and valuable niche for itself in today’s market. As consumer demand for sustainable and eco-friendly products continues to grow, companies like {} are well-positioned to thrive and lead the way in developing new and exciting applications for materials like cotton linter pulp.With its dedication to sustainability and innovation, {} is not only creating valuable new products and materials but is also helping to drive positive change in the industries it serves. As the demand for sustainable and eco-friendly products continues to grow, the company’s commitment to utilizing cotton linter pulp as a raw material offers a promising and exciting future for both the company and the industries it serves.
Read More
Top Uses and Benefits of Powdered Cellulose
Powdered Cellulose Used by {} to Enhance Food ProductsIn recent years, the use of powdered cellulose in food products has become increasingly popular. This natural ingredient is derived from plant fibers and is used as a bulking agent and anti-caking agent in a wide range of processed foods. One company at the forefront of utilizing powdered cellulose to enhance food products is {}.{} is a leading food manufacturer that specializes in creating high-quality, innovative products for consumers around the world. With a commitment to using only the best ingredients and cutting-edge technology, {} has embraced the use of powdered cellulose in many of its food offerings.Powdered cellulose, also known as cellulose powder, is made from finely ground cellulose fibers that are extracted from plants such as wood pulp, cotton, or other sources. It is a versatile ingredient that can be used in a variety of foods, including baked goods, dairy products, sauces, and dressings. As a bulking agent, powdered cellulose helps to improve the texture and mouthfeel of food products, while also providing a source of dietary fiber.In addition to its bulking properties, powdered cellulose is also used as an anti-caking agent in powdered food products. It helps to prevent clumping and ensures that the product remains free-flowing, making it easier for consumers to use and enjoy. With its natural origins and functional benefits, powdered cellulose has become an important ingredient for food manufacturers looking to enhance the quality and appeal of their products.{} has been using powdered cellulose in a variety of its food products, including shredded cheese, grated cheese, and powdered cheese blends. By incorporating this natural ingredient into its cheese products, {} has been able to improve texture and reduce caking, resulting in a better overall consumer experience.Furthermore, {} has used powdered cellulose to boost the fiber content of its food products. As consumers continue to seek out foods that are rich in fiber, the company has recognized the importance of incorporating this nutrient into its offerings. With the addition of powdered cellulose, {} has been able to create food products that not only taste great but also provide a good source of dietary fiber.{} is committed to ensuring that its food products meet the highest standards of quality and safety. The company works closely with suppliers to source the finest ingredients, including powdered cellulose, and conducts rigorous testing to ensure that its products meet or exceed regulatory standards. By integrating powdered cellulose into its food products, {} has been able to improve the overall quality and functionality of its offerings, while also meeting the evolving needs of consumers.As consumers continue to demand foods that are wholesome, nutritious, and free from artificial additives, the use of natural ingredients like powdered cellulose will likely become even more widespread. With its numerous functional benefits and natural origins, powdered cellulose has become an indispensable ingredient for food manufacturers looking to enhance the appeal and nutritional value of their products.Going forward, {} remains committed to exploring new ways to use powdered cellulose and other natural ingredients to create even more innovative and appealing food products. By staying at the forefront of ingredient innovation, the company aims to continue providing consumers with delicious, high-quality foods that they can feel good about enjoying.In conclusion, powdered cellulose has become an essential ingredient for {} in its efforts to create high-quality, innovative food products. By embracing the use of powdered cellulose, the company has been able to improve the texture, functionality, and nutritional value of its offerings, while also meeting the evolving needs and preferences of consumers. As the demand for natural, wholesome foods continues to grow, the use of powdered cellulose and other natural ingredients is expected to play an increasingly important role in the food industry.
Read More
Bulk Ethyl Alcohol Solution: News Update and Information
Ethyl Alcohol (Bulk Solution) Continues to Make Waves in the MarketIn recent years, the demand for ethyl alcohol (bulk solution) has been on the rise in various industries across the globe. From pharmaceuticals to personal care and even in the production of sanitizers, the versatile nature of ethyl alcohol has made it a widely sought-after product in the market. One company that has been at the forefront of meeting this demand is [Company Name]. With their commitment to quality and innovation, they have been making waves in the industry with their ethyl alcohol (bulk solution) product.[Company Name] is a leading supplier of ethyl alcohol (bulk solution) with a strong presence in the global market. The company takes pride in its state-of-the-art manufacturing facilities that adhere to the highest quality standards and strict regulatory requirements. This commitment to excellence has enabled them to consistently deliver premium quality ethyl alcohol (bulk solution) to their customers, gaining their trust and loyalty in the process.One of the key factors that set [Company Name] apart from its competitors is their dedication to research and development. They have a team of expert scientists and researchers who are constantly working on refining their processes and improving the quality of their products. This has allowed them to stay ahead of the curve in terms of product innovation, ensuring that they can meet the evolving needs of their customers.The ethyl alcohol (bulk solution) offered by [Company Name] is known for its purity and consistency. It is produced through a meticulous distillation process that removes impurities and contaminants, resulting in a product that meets the highest standards of quality. This has made it a preferred choice for various applications, including the manufacture of pharmaceuticals, cosmetics, and sanitizers.With the recent global health crisis, there has been an unprecedented demand for ethyl alcohol (bulk solution) for the production of hand sanitizers. [Company Name] has risen to the challenge by ramping up their production to meet this surge in demand. Their ability to scale up their operations while maintaining the quality and integrity of their product has been commendable, earning them the trust of their customers during this critical time.In addition to their commitment to quality, [Company Name] also places a strong emphasis on sustainability and environmental responsibility. They have implemented eco-friendly practices in their manufacturing processes, ensuring that they minimize their carbon footprint and contribute to a healthier planet. This has resonated well with their customers, who value their ethical approach to business.Looking ahead, [Company Name] has ambitious plans for the future of their ethyl alcohol (bulk solution) product line. They are exploring new avenues for growth and expansion, both geographically and in terms of product diversification. They are also investing in cutting-edge technologies to further enhance the quality and efficiency of their production processes, positioning themselves as a leader in the industry.As the demand for ethyl alcohol (bulk solution) continues to rise, [Company Name] is poised to play a pivotal role in meeting this demand and shaping the future of the market. With their unwavering commitment to quality, innovation, and sustainability, they are well-positioned to maintain their status as a trusted supplier of ethyl alcohol (bulk solution) for years to come.
Read More
Refined Cotton: Premium Quality Natural Fiber for Sustainable Textiles
Certainly! Please provide the company introduction and the news content about "C100 Refined Cotton" (excluding the brand name), and I will draft an 800-word news article for you.
Read More
Refined Cotton M30 – Premium Quality Cotton Material
Certainly! Please provide the company introduction you'd like me to incorporate into the news article, and I will draft an 800-word news piece about M30 Refined Cotton accordingly.
Read More
Understanding Regenerated Cellulose: What You Need to Know
[Company Name] Revolutionizes the Fashion Industry with Sustainable Regenerated Cellulose Fabric[Company Name], a leading innovator in the sustainable fashion industry, has recently introduced a new line of fabrics made from regenerated cellulose. This pioneering development is set to revolutionize the fashion industry by providing a more environmentally friendly alternative to traditional fabrics.Regenerated cellulose is a form of cellulose derived from plant-based materials such as wood pulp and cotton linters. The process of regenerating the cellulose involves breaking down the plant fibers and then reconstituting them into a durable and versatile fabric. This method of production significantly reduces the reliance on non-renewable resources and minimizes the environmental impact associated with fabric production.[Company Name] is at the forefront of this innovative technology, leading the way in creating sustainable and eco-friendly fabrics that meet the growing demand for ethical and environmentally conscious fashion. The company's commitment to sustainability is evident in its production processes, which prioritize the use of renewable energy and minimize water and chemical usage.The newly introduced regenerated cellulose fabric by [Company Name] offers a range of benefits that make it a desirable choice for both fashion designers and consumers. The fabric is breathable, lightweight, and has a luxurious feel, making it suitable for a wide range of clothing styles and applications. In addition, regenerated cellulose fabric has excellent draping qualities, making it ideal for creating elegant and fluid silhouettes in garments.One of the key advantages of regenerated cellulose fabric is its biodegradability. Unlike synthetic fabrics, which can take hundreds of years to decompose, regenerated cellulose fabric can naturally break down in a much shorter timeframe, significantly reducing its environmental impact at the end of its life cycle.Furthermore, [Company Name]'s regenerated cellulose fabric is produced using closed-loop manufacturing processes, which minimize waste and ensure that by-products are recycled and reused. This commitment to sustainable production practices aligns with the company's overarching goal of reducing its carbon footprint and contributing to a more sustainable fashion industry.The introduction of regenerated cellulose fabric by [Company Name] also reflects the growing consumer demand for sustainable and ethically produced fashion. As more consumers become aware of the environmental and social impact of the fashion industry, there is a growing interest in supporting brands that prioritize sustainability and ethical practices.[Company Name] is dedicated to meeting this demand by offering a wide range of regenerated cellulose fabric options that cater to the diverse needs of fashion designers and brands. Whether it's for creating everyday clothing, activewear, or high-end fashion pieces, the versatility and sustainability of regenerated cellulose fabric make it a highly sought-after choice in the fashion industry.In addition to its environmental benefits, regenerated cellulose fabric also supports the ethical treatment of workers in the supply chain. By prioritizing sustainable and responsible sourcing practices, [Company Name] ensures that the production of its regenerated cellulose fabric upholds the highest standards of social responsibility and fair labor practices.The introduction of regenerated cellulose fabric by [Company Name] underscores the company's ongoing commitment to driving positive change in the fashion industry. Through innovation and sustainability, [Company Name] is leading the way in transforming the way fashion is produced and consumed, setting a new standard for ethical and environmentally conscious fashion.As the fashion industry continues to evolve, [Company Name] is proud to be at the forefront of this movement, offering sustainable and luxurious options for designers and consumers who are passionate about making a positive impact on the environment and the future of fashion. With its regenerated cellulose fabric, [Company Name] is poised to make a lasting impression on the fashion industry and inspire a new era of sustainable and ethical fashion.
Read More
Exploring the Benefits of Cellulose Acetate for Various Applications
Cellulose Acetate is a versatile material that has been gaining popularity in various industries for its unique properties and usage. One company that has been at the forefront of utilizing Cellulose Acetate in innovative ways is [company name].[Company name] is a leading manufacturer and supplier of Cellulose Acetate products, specializing in the development and production of high-quality materials for a wide range of applications. The company has a strong reputation for its commitment to quality, innovation, and sustainability, making it a trusted partner for businesses looking for reliable and eco-friendly solutions.The use of Cellulose Acetate has seen a significant uptick in recent years, thanks to its versatility and environmentally-friendly nature. Cellulose Acetate is a semi-synthetic material made from purified cellulose, which is derived from wood pulp or cotton linters. It is known for its durability, chemical resistance, and biodegradability, making it an ideal choice for a variety of products and applications.One of the key industries that [company name] serves is the textiles and fashion industry. Cellulose Acetate is commonly used in the production of high-quality eyewear frames, as well as fashion accessories such as buttons, buckles, and jewelry. The material offers a lightweight and durable alternative to traditional plastics, and its biodegradability makes it an eco-friendly choice for environmentally-conscious consumers.In addition to its use in fashion, Cellulose Acetate is also gaining traction in the automotive industry. [Company name] provides Cellulose Acetate-based materials for automotive interiors, including dashboard components, door handles, and trim. The material's resistance to heat and chemicals, as well as its renewable and biodegradable nature, make it a sustainable and practical choice for automobile manufacturers.Another exciting application of Cellulose Acetate is in the realm of medical devices and pharmaceuticals. [Company name] develops and supplies Cellulose Acetate products for use in medical implants, drug delivery systems, and surgical instruments. The material's biocompatibility, low toxicity, and biodegradability make it a preferred choice for medical applications, meeting the stringent safety and regulatory requirements of the healthcare industry.Moreover, [company name] is also actively involved in the development of Cellulose Acetate-based packaging solutions for food and beverage products. The material's barrier properties, resistance to grease and oil, and ability to be recycled or composted make it a sustainable and suitable option for food packaging, reducing the environmental impact of single-use plastics.Additionally, Cellulose Acetate has also found its way into the world of electronics and technology. [Company name] provides Cellulose Acetate-based materials for electronic housings, casings, and components, offering a lightweight, durable, and environmentally-friendly alternative to traditional plastics.It is clear that the uses for Cellulose Acetate are diverse and widespread, and [company name] is leading the way in harnessing the full potential of this remarkable material. With a strong commitment to quality, innovation, and sustainability, the company is poised to continue driving the adoption of Cellulose Acetate across various industries, offering businesses and consumers alike a greener and more sustainable choice for their products.In conclusion, the use of Cellulose Acetate is on the rise, and [company name] is at the forefront of this trend, providing high-quality, sustainable materials for a wide range of applications. As industries continue to seek eco-friendly and innovative solutions, Cellulose Acetate is poised to play a central role in shaping the future of modern manufacturing. With [company name]'s expertise and dedication to excellence, the possibilities for Cellulose Acetate are endless, and its impact on the global economy and environment is sure to be profound.
Read More
High-Quality Nitrocellulose Manufacturer Expands Production Capacity
Certainly! Please provide the company introduction text that you would like me to incorporate.
Read More
Discover the Benefits of Powdered Cellulose for Various Products
Powdered Cellulose has long been used in the food industry as an anti-caking agent, stabilizer, and thickening agent. Made from plant fibers, it is not only a versatile ingredient but also a natural one. As more and more consumers seek out natural and clean-label products, the demand for powdered cellulose has been on the rise.One company at the forefront of meeting this demand is {}. With a strong focus on innovation and sustainability, {} has become a leading supplier of powdered cellulose to the food industry. The company's commitment to quality and its ability to tailor its products to meet the specific needs of its customers have set it apart in the market.Established in [], {} has quickly established itself as a trusted supplier in the industry. The company's state-of-the-art production facilities and strict quality control measures ensure that its powdered cellulose meets the highest standards. In addition to its commitment to quality, {} is also dedicated to sustainability. The company works closely with its suppliers to source the finest raw materials in a responsible and sustainable manner.One of the key advantages of {}'s powdered cellulose is its versatility. It can be used in a wide range of applications, including baked goods, dairy products, sauces, and dressings. Its ability to improve texture, stability, and shelf-life makes it an invaluable ingredient for food manufacturers. Additionally, powdered cellulose is an excellent source of dietary fiber, making it an attractive option for companies looking to enhance the nutritional profile of their products.Another factor that sets {} apart is its ability to customize its products to meet the specific needs of its customers. Whether a food manufacturer requires a specific particle size, density, or functionality, {} has the expertise and capability to deliver tailored solutions. This level of flexibility and attention to detail has earned the company a loyal customer base and a reputation for excellence in the industry.In response to the growing demand for natural and clean-label products, {} has continued to invest in research and development. The company is constantly exploring new applications for powdered cellulose and finding innovative ways to enhance its performance. By staying ahead of the curve, {} is well-positioned to meet the evolving needs of the food industry and its customers.Looking to the future, {} is committed to further expanding its presence in the market. With a focus on sustainability, innovation, and customer satisfaction, the company is well-equipped to continue leading the way in the supply of powdered cellulose. By maintaining its high standards and dedication to excellence, {} is poised for continued success in the years to come.
Read More
High-Quality Cotton Linter Paper for Durable and Eco-Friendly Applications
Certainly! Please provide the specific news content about Cotton Linter Paper and the company introduction you'd like me to incorporate, so I can craft the 800-word news article for you.
Read More